Bowl Elevator for Controlled Upward Feeding
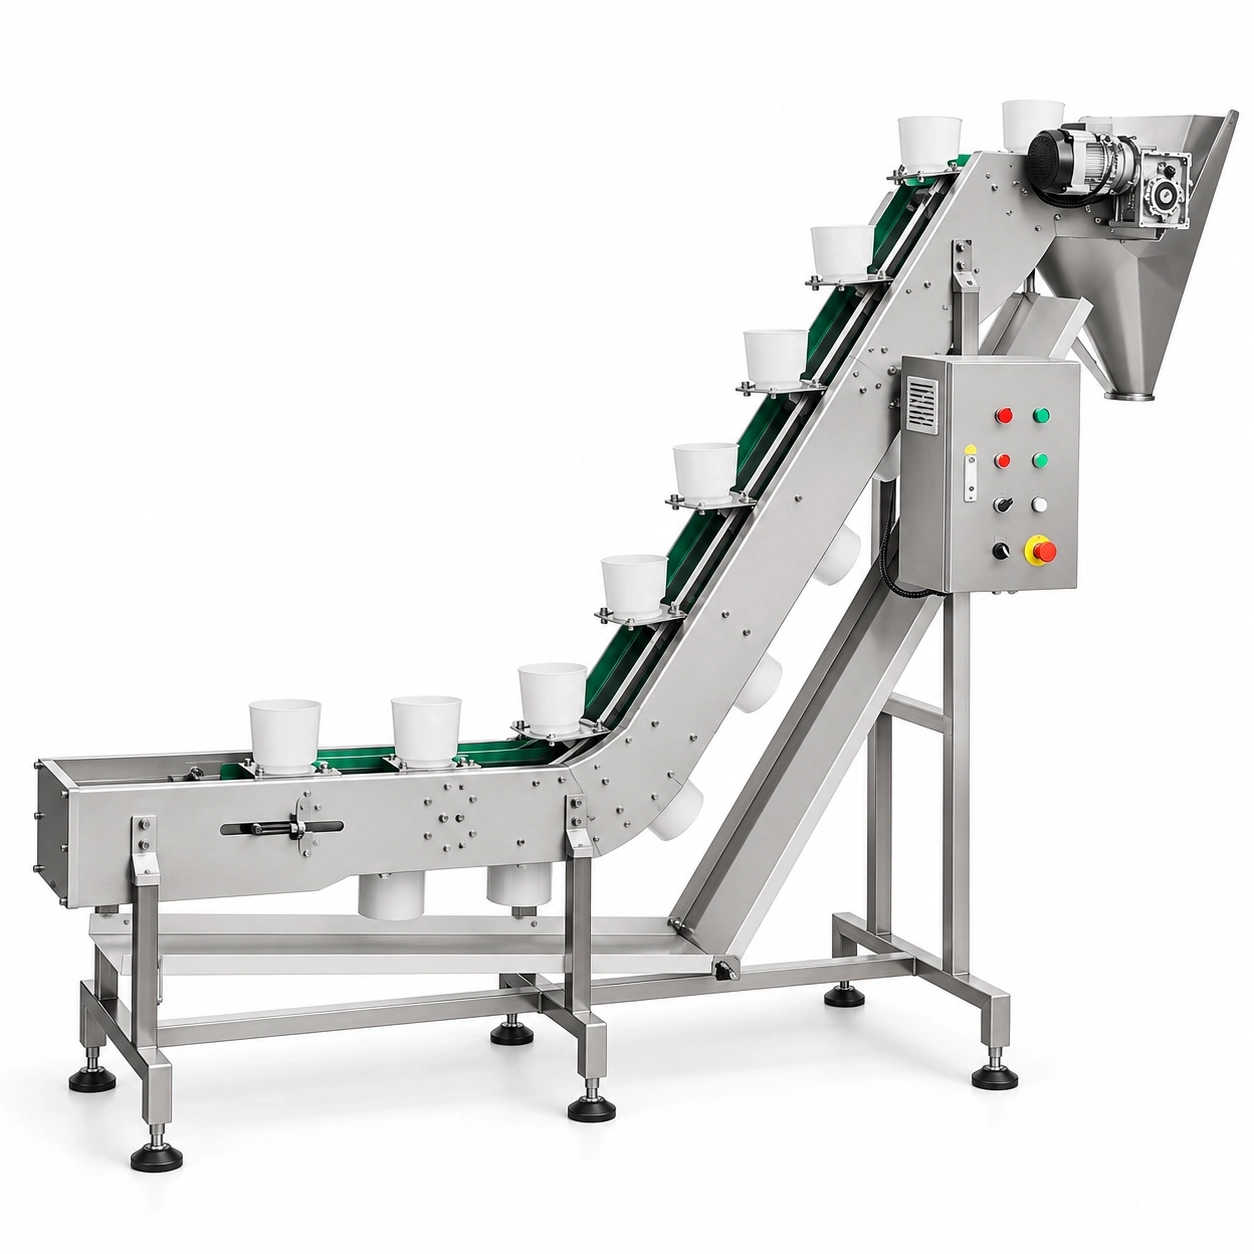
The Bowl Elevator is an inclined feeding conveyor for moving compatible products upward in separate bowl carriers. Rather than using one flat transport surface, the Bowl Elevator provides a defined space for each portion as it moves from the feed point toward the next packaging stage. This carrier-based arrangement can suit projects where product behavior, feed height, and the downstream machine require a controlled upward transfer. The documented configuration is the WT-170 1.4L model. It can be considered as a feeding component before compatible weighing or packaging equipment, with the final arrangement matched to the material and the surrounding line layout.
WT-170 1.4L Listed Specifications
| Item |
Listed specification |
| Model |
WT-170 1.4L |
| Power |
0.75 kW |
| Single-bowl capacity |
1.4 L |
| Conveying capacity |
2.5 m³/h |
These listed values describe the documented Bowl Elevator configuration. The 1.4 L figure is the stated capacity of one bowl, while 2.5 m³/h is the listed conveying-capacity value for the equipment. They describe different aspects of the Bowl Elevator and should be read in that context. The 0.75 kW value is the supplied power specification. Together, these figures provide a starting point for discussing feed duty, available space, and the relationship between product supply and downstream demand.
Key Bowl Elevator Features
-
Discrete bowl carriers: Each carrier provides a defined space for product during upward movement and supports a clear transfer path from feed to discharge.
-
Inclined conveying arrangement: The Bowl Elevator is configured for upward transfer where the next process is above the incoming feed level.
-
Documented carrier capacity: The WT-170 1.4L model has a stated single-bowl capacity of 1.4 L for early product-handling discussions.
-
Listed conveying reference: The supplied 2.5 m³/h conveying-capacity figure provides a reference when reviewing feed requirements.
-
Packaging-line interface: The Bowl Elevator can be reviewed as a feeding stage ahead of compatible weighing or packaging equipment.
These features describe the function of the Bowl Elevator without assuming every product behaves in the same way. A bowl that suits one portion shape may need a different loading approach for another. The practical question is whether product enters, travels, and leaves the carrier in a stable manner for the intended line. This movement should be understood when the Bowl Elevator connects an upstream supply point to an automated packaging stage.
Applications for Product Feeding
Feeding a rice flour packaging machine
A Bowl Elevator may be reviewed as an upward feeding component for a rice flour packaging machine when the material and process arrangement suit bowl-based conveying. Product filling behavior, desired feed elevation, and the receiving point should be discussed together. The listed Bowl Elevator specifications provide a product reference, while the line arrangement should reflect the material flow required by the packaging machine.
Supporting a cream filling machine line
In a system that includes a cream filling machine, a Bowl Elevator may be considered when compatible product portions need to reach a higher feed point before a connected stage. Suitability depends on the actual material and how it can be handled in the documented bowl carriers. Share product characteristics and the required transfer sequence so the Bowl Elevator can be discussed in relation to the process.
Upstream handling for packaging for fresh herbs
For packaging for fresh herbs, a Bowl Elevator can be reviewed where product can be conveyed in individual bowls and the inclined path fits the planned process. Fresh or delicate products may require attention to loading, settling in the carrier, and transfer at discharge. The Bowl Elevator provides the upward conveying function; the final application should be matched to product condition and the next packaging operation.
Planning the Line Interface
The Bowl Elevator is one link in a connected packaging line. First identify the incoming product condition and how material reaches the lower feed point. Next consider required elevation, bowl loading pattern, and the location of the receiving machine. Finally, review how product leaves the Bowl Elevator and enters the following stage. This sequence supports a clear handoff between equipment and practical access around the inclined conveyor.
Installation space also matters. The Bowl Elevator needs practical access to its feed area, inclined route, and discharge point. Consider space around the equipment for normal operation and cleaning, together with adjacent machines. A layout discussion benefits from product dimensions, approximate product quantity, required feed elevation, and receiving-stage details. These inputs allow the Bowl Elevator to be considered as part of the overall material path.
Why Choose This Bowl Elevator Configuration
The WT-170 1.4L Bowl Elevator combines a carrier-based upward conveying concept with stated reference specifications: 0.75 kW power, 1.4 L per bowl, and 2.5 m³/h conveying capacity. This gives visitors a direct basis for understanding the equipment and how it may support a packaging line. Its value lies in creating a defined upward route for compatible products before they reach a weighing or packaging machine.
For an inquiry, provide product type, approximate dimensions, shape, fragility, required feed elevation, and the equipment that receives the product. This information helps position the Bowl Elevator within the intended process and supports discussion of a suitable feed and discharge arrangement. The Bowl Elevator can then be reviewed against the actual product flow rather than as a generic conveyor alone.
Frequently Asked Questions
What is the capacity of one bowl?
The documented WT-170 1.4L Bowl Elevator has a stated single-bowl capacity of 1.4 L.
What does the 2.5 m³/h figure describe?
It is the listed conveying-capacity value for the Bowl Elevator. Practical material flow also depends on how the actual product fills and leaves the bowls.
What information is helpful before selecting a Bowl Elevator?
Please share product size, shape, fragility, target feed elevation, and the required receiving stage. These details help relate the Bowl Elevator to the intended packaging-line arrangement.

 EN